
|
01
|
Air Bubbles and Surface Defects in Complex Shoe Upper Textures
Bubble formation mechanism:
High viscosity trapping: KPU polyurethane raw materials (Polyester polyol A and Isocyanate B) easily trap air during proportioning and stirring. Incomplete degassing: Without high-speed vacuum treatment during mold filling, micro-bubbles remain inside fine 3D shoe upper cavities, resulting in surface pinholes and high scrap rates. Poor fluidity: If raw materials are not preheated to the optimal 30–40°C range, uneven flow leads to incomplete filling at thin edges. |
|
02
|
Unstable Mesh Lamination, Delamination, and Glue Overflow
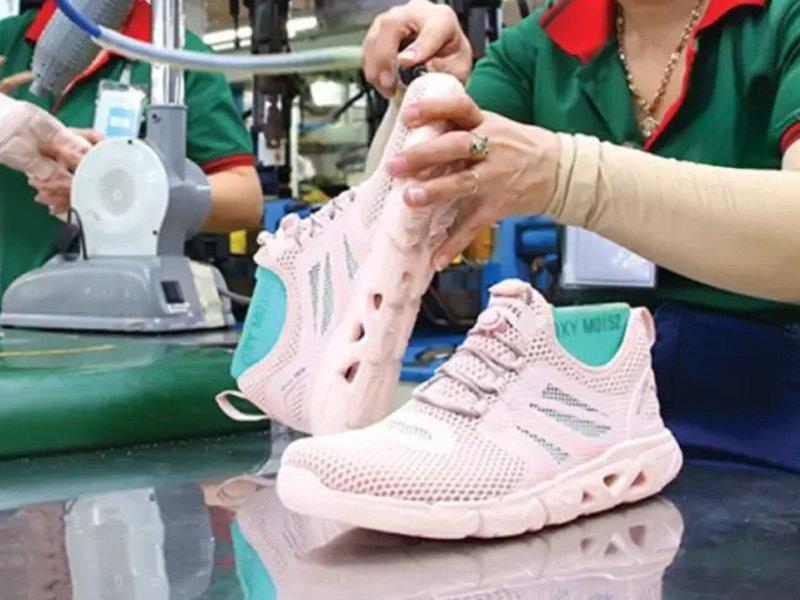
KPU shoe uppers require a firm bond between the molded polyurethane layer and the breathable shoe mesh fabric.
Peeling and delamination: If the preliminary plasticizing degree in the curing tunnel is inaccurate—either over-cured or under-cured—the KPU layer fails to bond firmly with the mesh during hot-pressing. Glue penetration & overflow: Uneven hydraulic pressure or temperature fluctuations during molding cause raw material to penetrate through the mesh fabric, ruining the appearance and flexibility of the shoe upper. Yellowing and aging: Improper baking temperatures during final curing lead to color distortion and reduced folding endurance. |
|
03
|
Strict Multi-Stage Process Windows and Low Manual Efficiency
Sensitive metering & mixing:
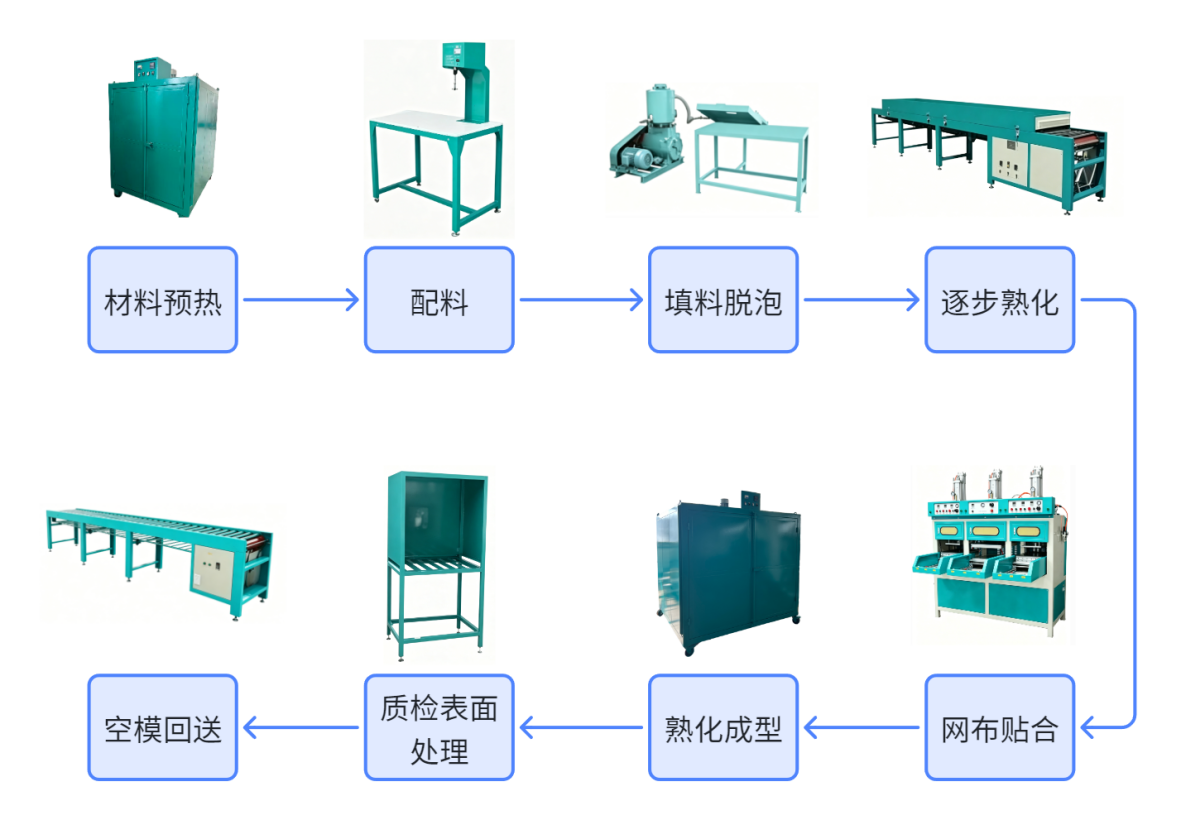
KPU formulation requires a strict 100:85–110 ratio and ±0.1% metering accuracy; manual proportioning easily causes batch-to-batch hardness deviations. Multi-step coordination bottlenecks: The 9-step process—from material preheating, mixing, release agent spraying, vacuum degassing, tunnel plasticizing, mesh lamination, oven curing, to mold return—requires seamless closed-loop circulation. High labor intensity: Without automated tunnel curing and mold return conveyor lines, manual mold handling is slow, labor-intensive, and prone to operational errors. |
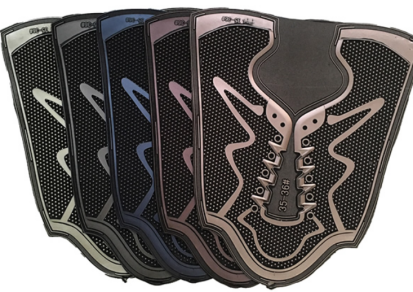
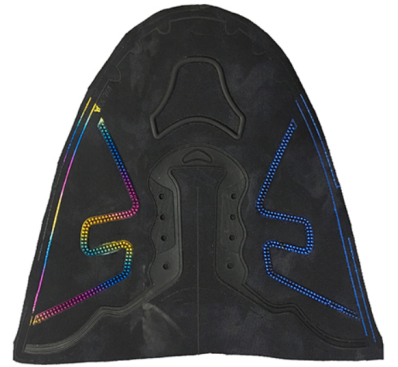
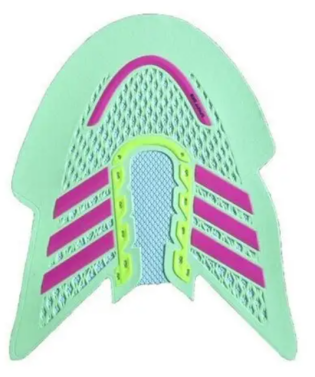
Haifeng Automation provides a complete turnkey KPU Shoe Upper Production Line Solution integrating raw material preheating, high-precision servo metering (±0.1%), high-speed vacuum degassing, tunnel preliminary plasticizing, 3-station/6-station hydraulic hot-press mesh lamination, constant-temperature curing, and closed-loop mold return. Equipped with Shenzhen Inovance PLC control systems, servo metering pumps with planetary reducers, and independent temperature control modules, the line ensures bubble-free 3D textures, strong mesh adhesion, and stable output of up to 288–352 pcs per 8-hour shift per molding unit.
Raw Materials & Formulation:
KPU polyurethane raw materials (Material A: Polyester polyol / Material B: Isocyanate, optional color paste addition).
Approximate raw material ratio: 100 : 85–110.
Raw material preheating temperature: 30–40°C (Remark: Requires one raw material drying oven).
Other ingredients: Release agent (Function: prevents adhesion), Pigment (Function: for coloring), (MC) Dichloromethane (Function: cleans mixing head), (DOP) Dioctyl phthalate (Function: cleans material tanks).
Pouring Capacity:
Maximum instantaneous flow rate: 10–30 g/s.
Metering accuracy: ±0.1%.
Equipment Specifications:
Operation Mode: Manual or semi-automatic control via Human-Machine Interface (HMI).
Machine Color: Standard industrial color.
Number of Workstations: 3 stations or 6 stations.
Heating Method: Water heating or oil heating (determined by specific process and environmental conditions).
| Step | Detailed Description | Equipment & Function | Corresponding Step Image |
|---|---|---|---|
| 1 | Material Preheating | Preheating Oven: Preheats the KPU raw materials so that the material reaches a temperature state suitable for processing, preparing for subsequent operations. | 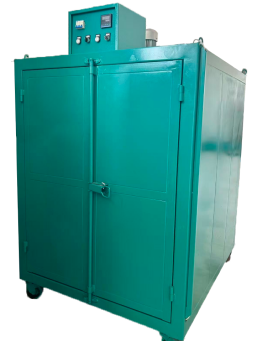 |
| 2 | Ingredient Mixing | Mixing Workbench: Proportions KPU raw materials according to the formula ratio and stirs evenly to ensure uniform mixing of raw material components. | 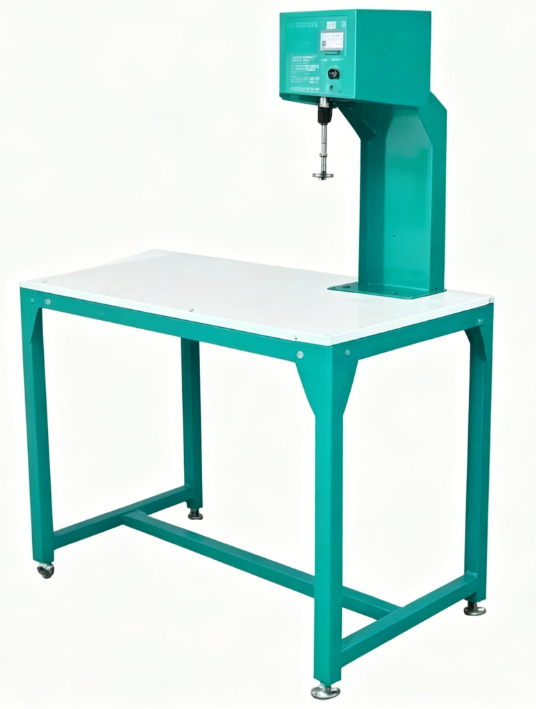 |
| 3 | Release Agent Spraying | Release Agent Spray Gun: Forms an isolation barrier to prevent materials from adhering to each other. | 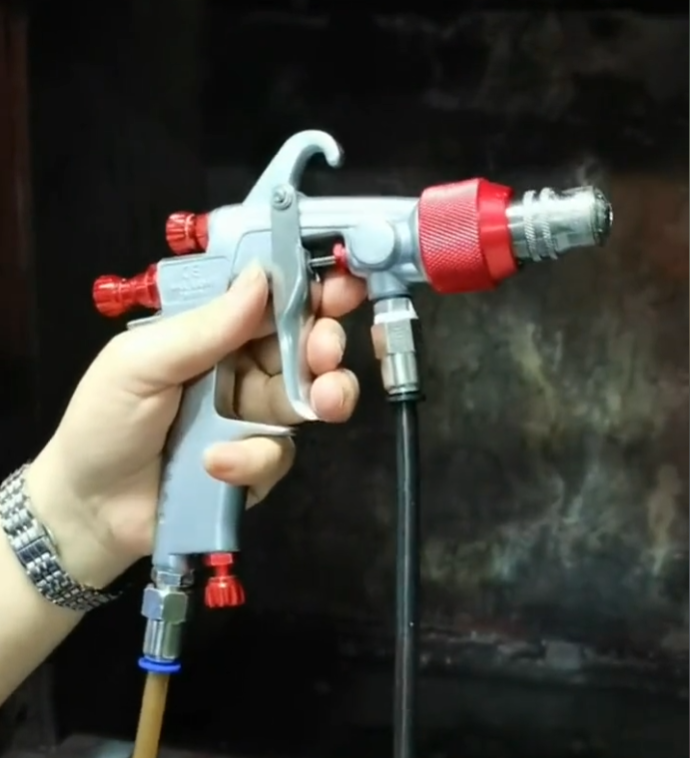 |
| 4 | Filling & Vacuum Degassing | High-Speed Vacuum Machine: Fills the prepared raw materials into the mold and removes air bubbles in the raw materials through vacuum treatment to avoid defects in finished products. | 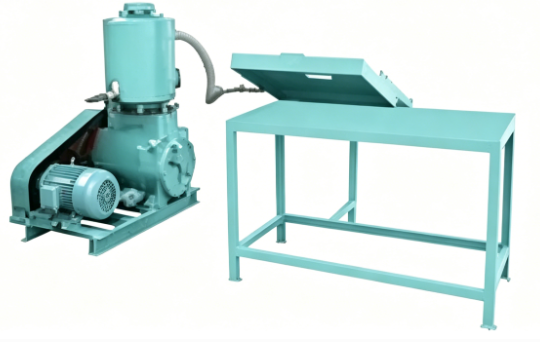 |
| 5 | Preliminary Plasticizing | Curing Line: Performs preliminary curing on the raw materials in the mold through a heating tunnel to shape the material into a semi-finished product. | 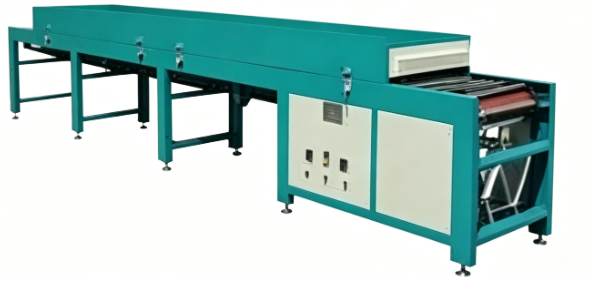 |
| 6 | Mesh Lamination | Molding Machine: Hot-presses and laminates the KPU semi-finished product with shoe mesh fabric to form a shoe material structure with mesh. | 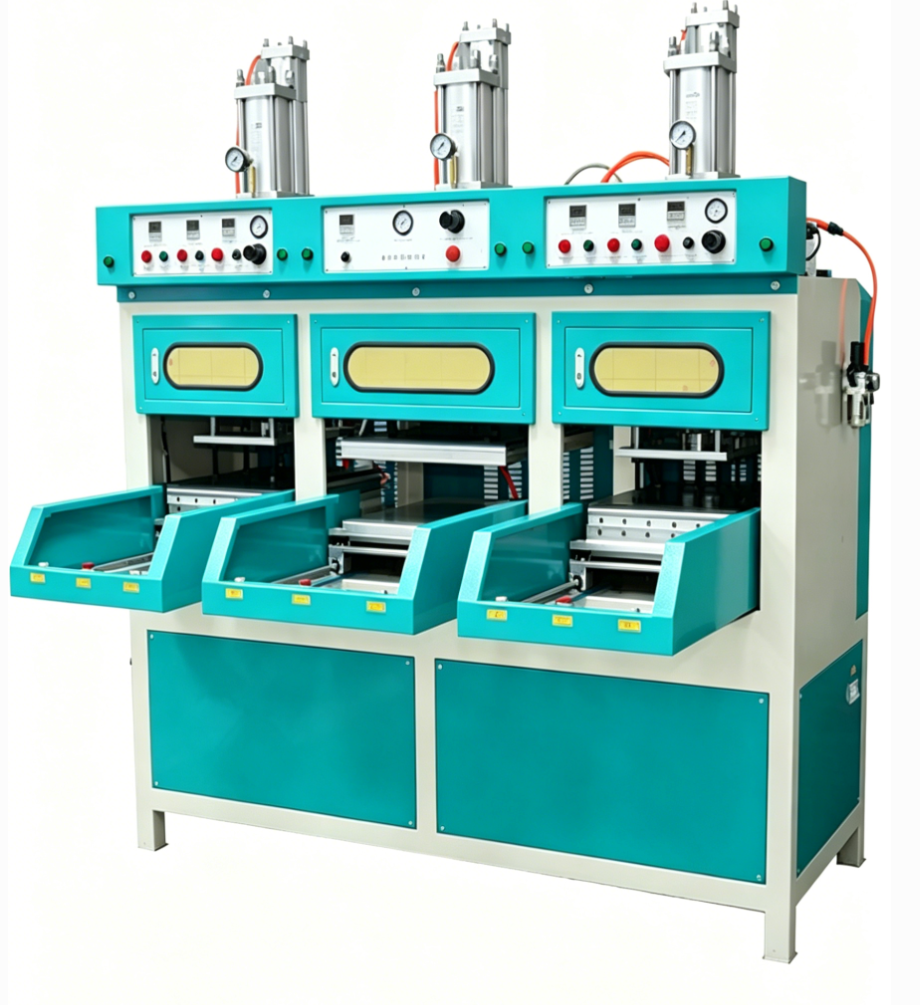 |
| 7 | Curing & Shaping | KPU Curing Oven & KPU Turnover Trolley: Places the laminated semi-finished products into the oven for curing treatment so that the material is completely solidified and shaped; the turnover trolley is used for batch transfer of semi-finished products. | 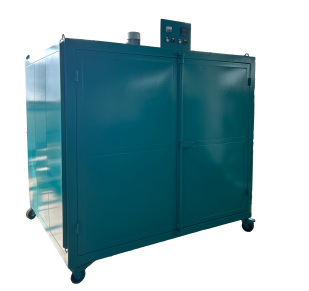 |
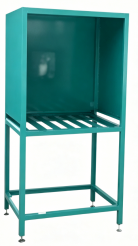
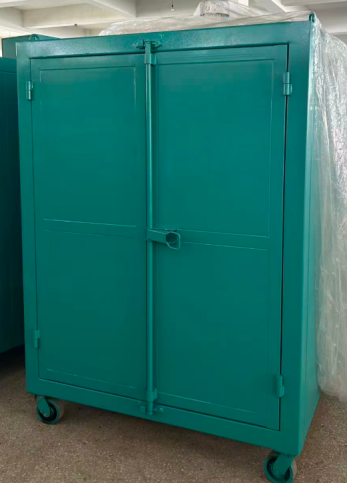
| 8 | QC & Mold Surface Treatment | Mold Treatment Cabinet: Comprehensive quality inspection; cleans and maintains production molds to ensure good mold condition and guarantee finished product quality in subsequent production. |
  |
| 9 | Empty Mold Return | Mold Return Line: Sends the empty molds after production back to the front-end process to enter the next production cycle. | 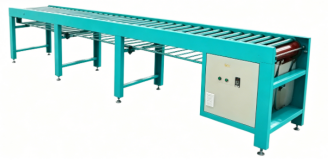 |
| No. | Name | Quantity | Dimensions (Approx., Unit: mm) | Unit Price (USD) |
|---|---|---|---|---|
| 1 | KPU Preheating Oven | 1 Set | Approx. (Ref. similar oven size) 1000×800×1500 |
|
| 2 | KPU Mixing Workbench | 1 Set | Approx. 1000×800×1100 | |
| 3 | KPU High-Speed Vacuum Machine | 1 Set | Approx. 1800×1000×2000 | |
| 4 | KPU Mold Return Line | 1 Set | Approx. 3000×800×1000 | |
| 5 | KPU Curing Line | 1 Set | Approx. 3500×800×1200 | |
| 6 | KPU Molding Machine | 1 Set | Approx. 2000×800×2350 | |
| 7 | KPU Mold Treatment Cabinet | 1 Set | Approx. 800×600×1500 | |
| 8 | KPU Curing Oven | 1 Set | Approx. 1700×1360×2050 | |
| 9 | KPU Turnover Trolley | 1 Set | Approx. 1200×800×1800 | |
| 10 | Release Agent Spray Gun | 1 Set | Approx. 105×155 |
| Category | Component Name | Model / Spec | Remarks |
|---|---|---|---|
| Pouring System | Metering System | Component A: 20cc High-precision metering pump | Motor is 1.3KW servo motor with planetary reducer |
| Component B: 20cc High-precision metering pump | Motor is 1.3KW servo motor with planetary reducer | ||
| Color Dosing System | 0.6cc High-precision metering pump | Drive motor is 0.75KW servo motor, 50L storage tank | |
| Mixing Head System | Needle valve mixing head | With independent cooling system | |
| Temperature Control System | Heating water tank | ||
| Material tank temperature | Independently control material tank temperature | ||
| 2 HP Water Chiller | Mixing head cooling | ||
| Mixing Head Cleaning System | 20L cleaning tank | ||
| Control System | PLC & Modules | Brand: Shenzhen Inovance H3U series PLC & modules | |
| 10-inch Touch Screen | Brand: MCGS | ||
| Low Voltage Electricals | Brand: DELIXI | ||
| Sensors | Brand: Inovance | ||
| Mold Release Spray Gun | Model: MRS-R/F, Brand: Taiwan Baoli, Spray width ±20 | Air pressure: 2.0Mpa, Weight: 320g | |
| Auxiliary Equipment | KPU Preheating Oven | Material preheating oven | Used for raw material preheating to improve molding fluidity |
| KPU Mixing Workbench | Raw material mixing table | Polyurethane A/B material mixing and proportioning | |
| KPU High-Speed Vacuum Machine | High-speed vacuum degassing machine | Filling and degassing to eliminate bubbles in finished products | |
| KPU Curing Line | Tunnel curing line | Preliminary plasticizing and shaping | |
| KPU Molding Machine | Shoe upper molding host machine | Mesh lamination and hot-press molding | |
| KPU Mold Return Line | Mold return conveyor line | Empty mold return to form closed-loop production | |
| KPU Mold Treatment Cabinet | Mold treatment cabinet | Mold cleaning and release agent spraying | |
| KPU Curing Oven | Maturing & curing oven | Constant temperature curing to enhance material properties | |
| KPU Turnover Trolley | Material turnover trolley | Finished product / mold turnover | |
| Air Storage Tank | 500×500×2000mm | Provides stable air source for pneumatic components | |
| Raw Material Oven | 1700×1360×2050mm | Dehumidification and drying of polyurethane raw materials | |
| Water Chiller | 900×600×1100mm | Mixing head and mold cooling | |
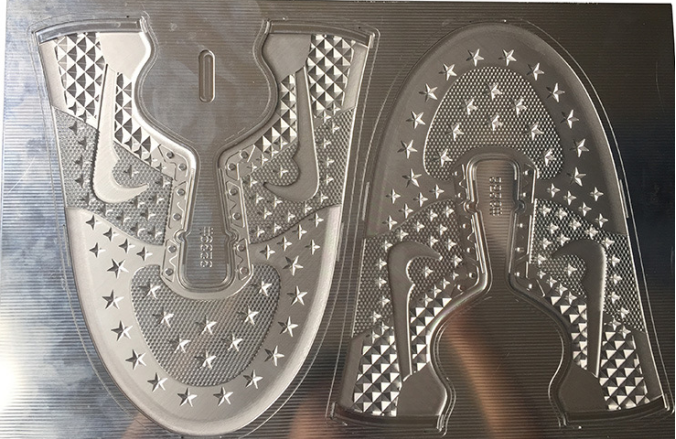
| Function: First select the mold for the product to be manufactured (unified standard mold). Materials: Aluminum alloy, Cr12MoV alloy tool steel. |
 |
| Function: Raw material oven for preheating and melting A/B materials. Model: XHG×3-2.5; Volume: 2.5 m³; Temperature setting range: 90°C; Temperature control mode: Automatic; Total power: 6.55 kW. |
 |
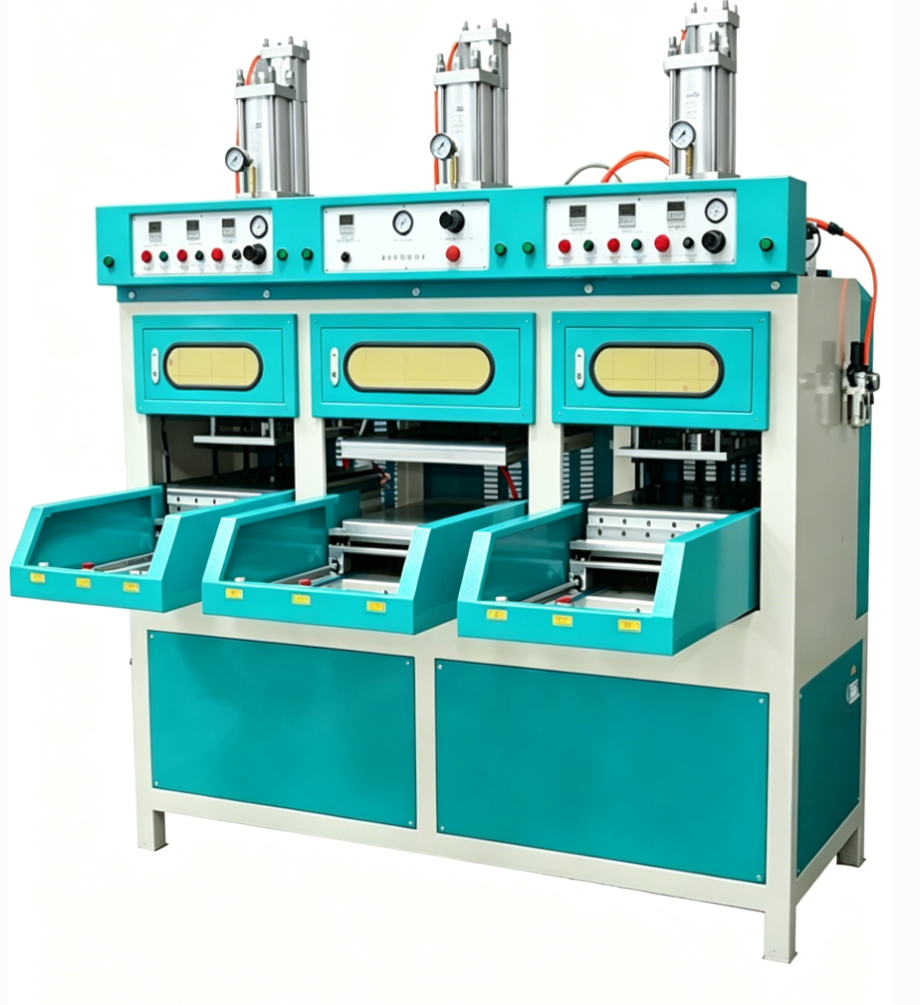
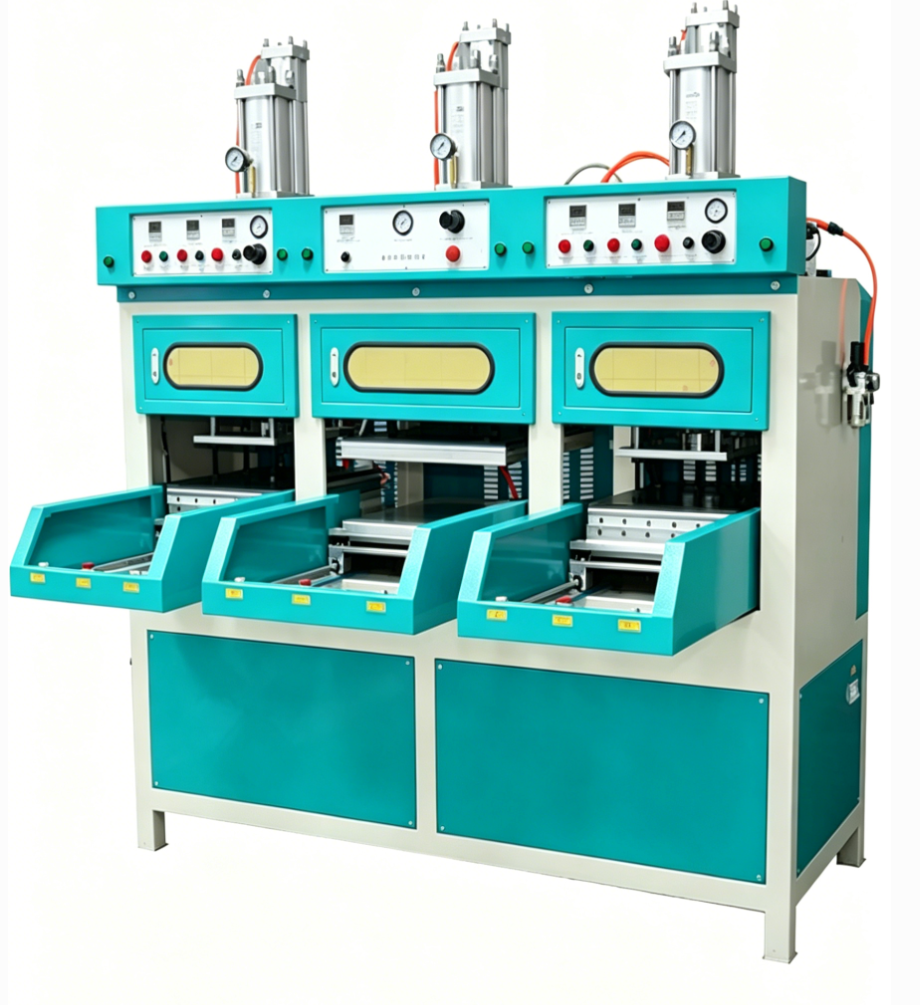
| Function: Shoe upper cover / shoe upper surface molding. Drive mode: Hydraulic drive; Voltage: 220/380V; Power: 30–50 kW; Number of stations: 3 stations. |
 |
| Function: Spraying release agent onto the mold before pouring. | 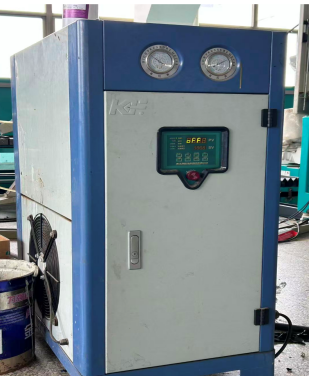 |
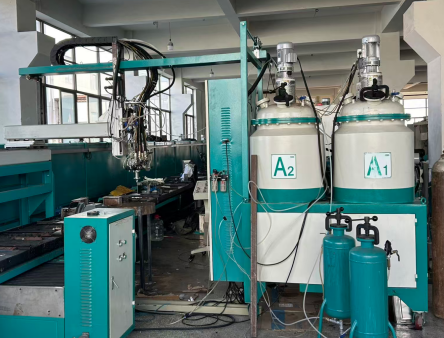
| Function: The pouring machine performs pouring based on the selected formula. Maximum instantaneous flow rate: 70 g/s; Rated voltage: 380V; Metering accuracy: ±0.5‰; Power phase: 3-phase; Metering pump speed adjustment range: 30–150 rpm; Mixing head speed: 8600±150 rpm; Rated frequency: 50 Hz; Adopts servo motor with planetary reducer; Electrical control system cabinet; Material tank material: Stainless steel, capacity: 120–220L (customizable according to customer needs). |
 |
| Function: Conveying molds smoothly across the curing and return cycle. | 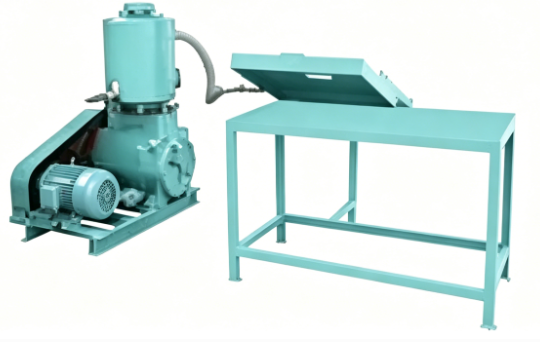 |
| Function: Used for cooling the pouring head and mixing chamber. Power: 1.91 kW. |
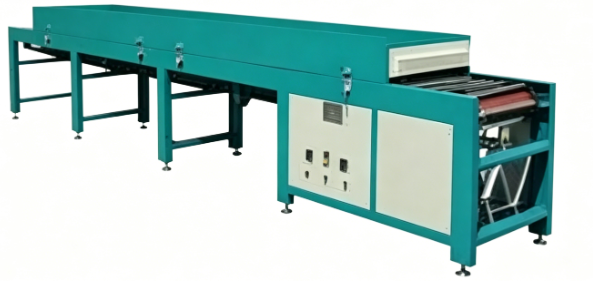 |
| Functions: Cleaning and valve control provide power and cooling source air pressure for the pneumatic system and nozzle cooling (requires continuous power supply). Power: 22 kW. |
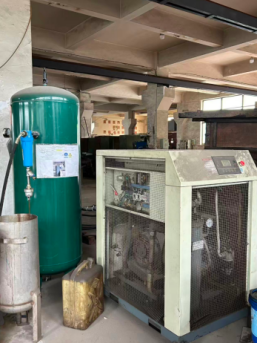 |
| Function: Mixing and proportioning of polyurethane A/B materials. | 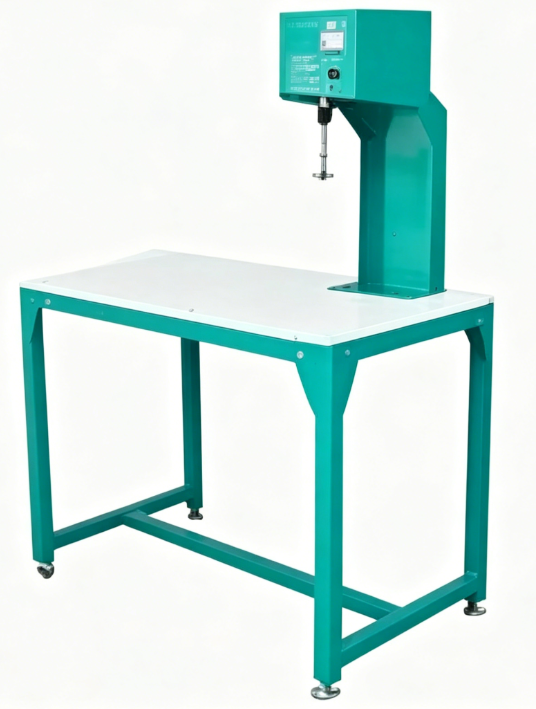 |
| Item | 1-Out-2 Mold | 1-Out-4 Mold |
|---|---|---|
| Single Mold Cycle Time | 5–8 minutes (Average: 6.5 minutes) | |
| Hourly Output | 18–22 pcs | 36–44 pcs |
| Daily Output (8 Hours) | 144–176 pcs / unit | 288–352 pcs / unit |
| Item | Requirements & Specifications |
|---|---|
| Workshop Requirements | Level ground (Area approx. 8m × 6m), Power supply, Compressed air, Cooling water, Ventilation |
| Temperature & Humidity | ≤40°C, Non-condensing environment |
| Power Supply | 3×380V ± 5%, 50Hz, Reliable grounding (Provided according to actual site needs) |
| Operators | 4–6 trained operators |
| 4. Energy Consumption (Installed Power) | Total main power: approx. 34 kW; Total power of other auxiliary equipment: approx. 25 kW |
| 5. After-Sales Service |
Technical Documentation: Operation manual, electrical diagrams, layout drawings. Installation & Training: Dispatch engineers for installation and training (expenses borne by the buyer). Warranty: 12 months from the date of delivery; free spare parts provided for quality issues (non-human damage). Long-Term Support: Technical guidance and spare parts supply provided after the warranty period. |
Full-Process Automated Production System

Comprehensive Quality Verification and Compliance Assurance