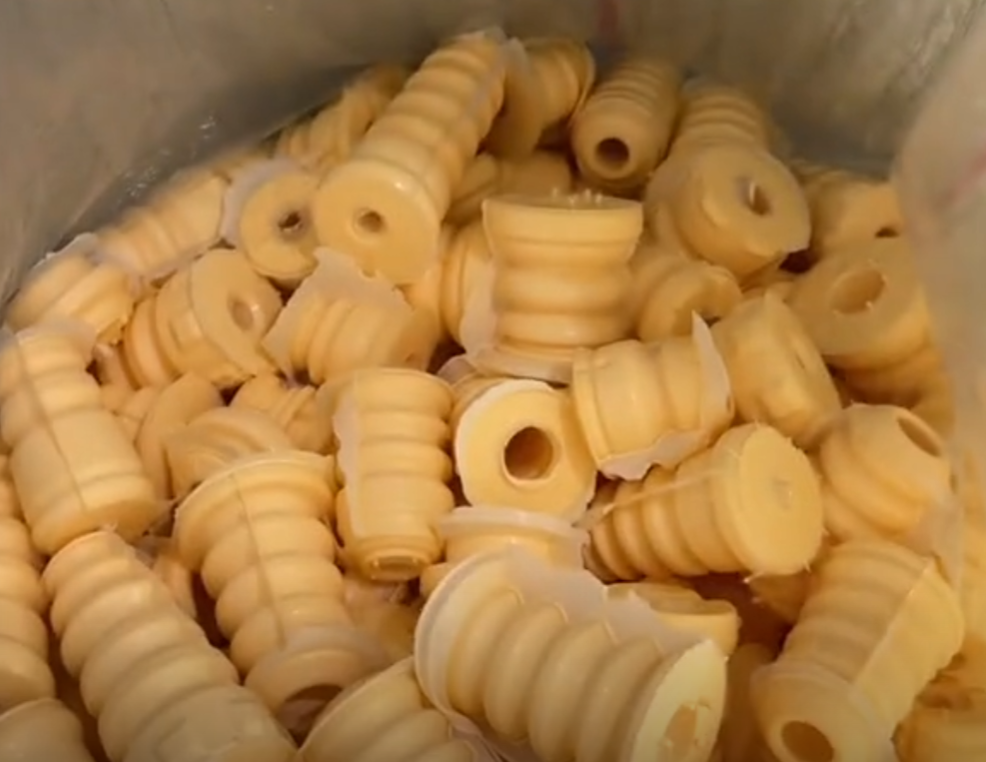
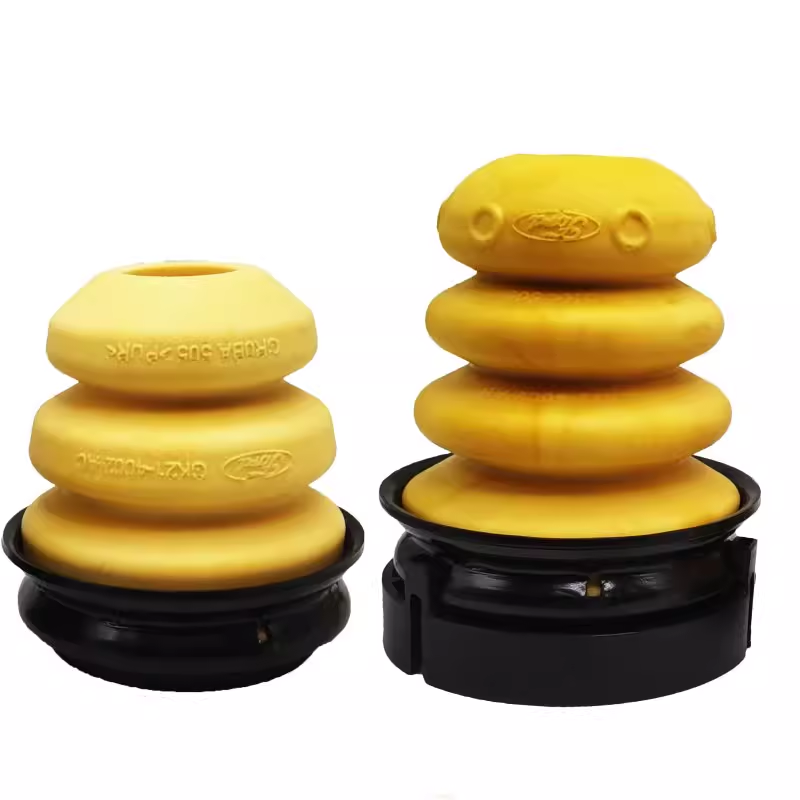
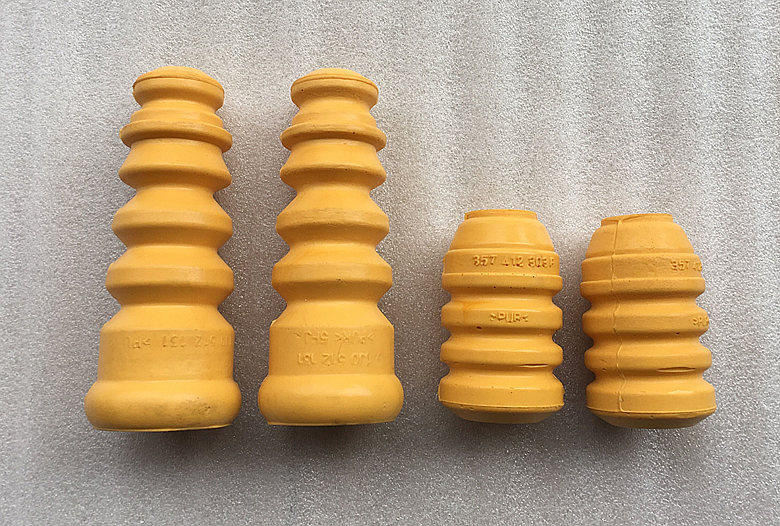
Polyurethane automotive shock absorber disc solution

Industry Pain Points

01

Creeper Deformation and Dimensional Stability (Material Fatigue)

Creep mechanism:

Phase 1 (Initial Creep):

Poor uniformity:Rapid deformation occurring within hours or days after installation (accounting for 30–50% of total creep)

Stage 2 (Secondary Creep):Stable, gradual deformation over a period ranging from several months to several years, which accounts for the majority of the service life.

Stage 3 (Final Creep):

Accelerated deformation under high stress and high temperature until failure.

02

Material Aging and Surface Cracking

As a polymeric material, polyurethane inherently has the drawback of insufficient resistance to aging.

Surface cracking:

After prolonged use, exposure to ultraviolet rays, ozone, and cyclic temperature and humidity fluctuations causes microcracks to form on the surface, which subsequently develop into through-cracks.

Rebound damping:

The cellular structure collapses after repeated compression, resulting in a decrease in cushioning capacity.

Rebound damping:

During high-speed compression, internal friction generates heat, and the accumulation of heat leads to a deterioration in material properties.

03

Extremely narrow process windows and monopolies on high-end materials

Reaction speed is too fast:

The NDI system has an extremely short reaction time (completed within seconds), and the raw materials tend to cure and clog the mixing chamber.

Sensitive to process parameters:

Even the slightest fluctuations in temperature, pressure, or mixing ratios can result in product scrap.

Technology Monopoly:

Currently, this sector is primarily controlled by foreign manufacturers such as Germany's BASF, including material formulations and production processes

Core of the Solution

Haifeng Automation, a veteran in the polyurethane automation equipment industry, focuses on the core demands of “comprehensive protection, long-lasting durability, green environmental protection, and intelligent efficiency”. It integrates independently accumulated solvent-free/water-based PU technology, precision manufacturing processes, and intelligent quality control systems, integrating core equipment and process solutions into the entire industrial chain of safety shoes. Leveraging technical experience in PU foaming equipment, precision metering systems, and other fields, it achieves four core goals, adapts to multi-scenario needs, and provides integrated “technical solution + equipment implementation” services.

Core Solution Modules

R&D of Scenario-Specific Specialized Materials

Ingredients and formulation:

PU polyurethane raw materials (Material A is generally polyester polyol; Material B is generally isocyanate)

The approximate ratio of the ingredients is 100:80–120.

Raw material preheating temperature: 35–45°C (Note: A raw material oven is required.)

Other ingredients: Demolding agent (function: prevent adhesion), pigment (function: for coloring), (MC) dichloromethane (function: clean the nozzle), (DOP) dioctyl phthalate (function: clean the tank).

Castability:

Maximum instantaneous flow rate: 20–40 g/s.

Measurement accuracy: ±0.1%.

Number of workstations:

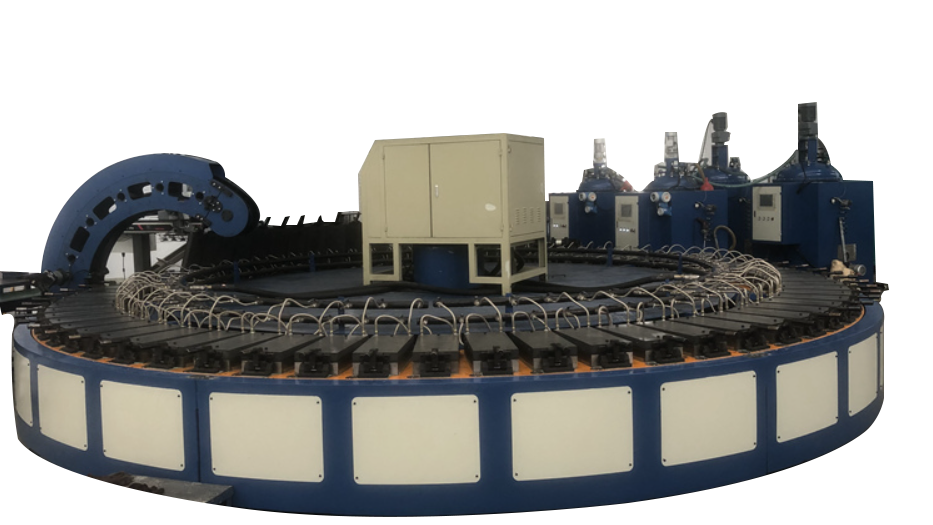
108 workstations (diameter 9.5 m) or 77 workstations (diameter 6.5 m).

Specific Process

Step Detailed Description Corresponding Step Image
1 Place inserts or skeletons into the mold
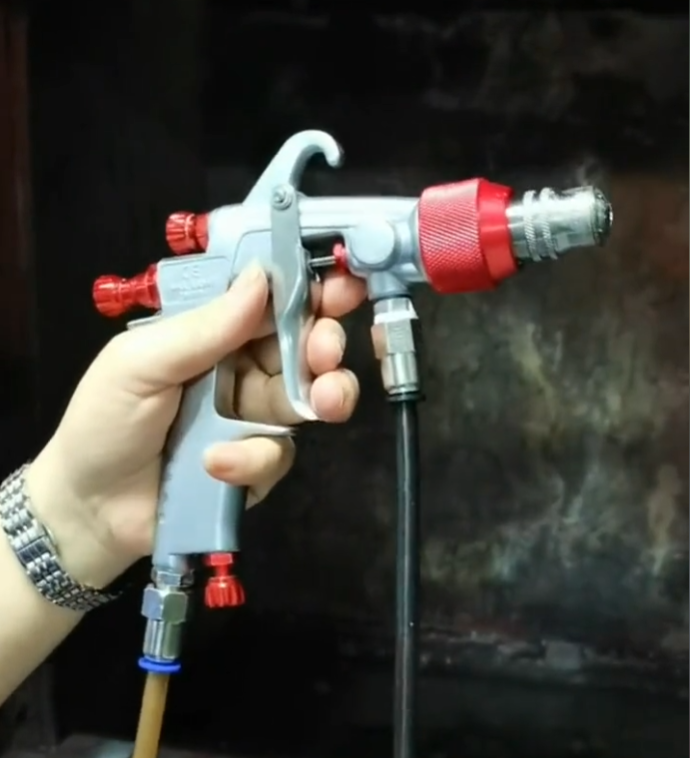
2 Automatically spray release agent
(If the mold cavity is complex, manual touch-up with a spray gun may be required)
3 Polyurethane pouring machine automatically pours
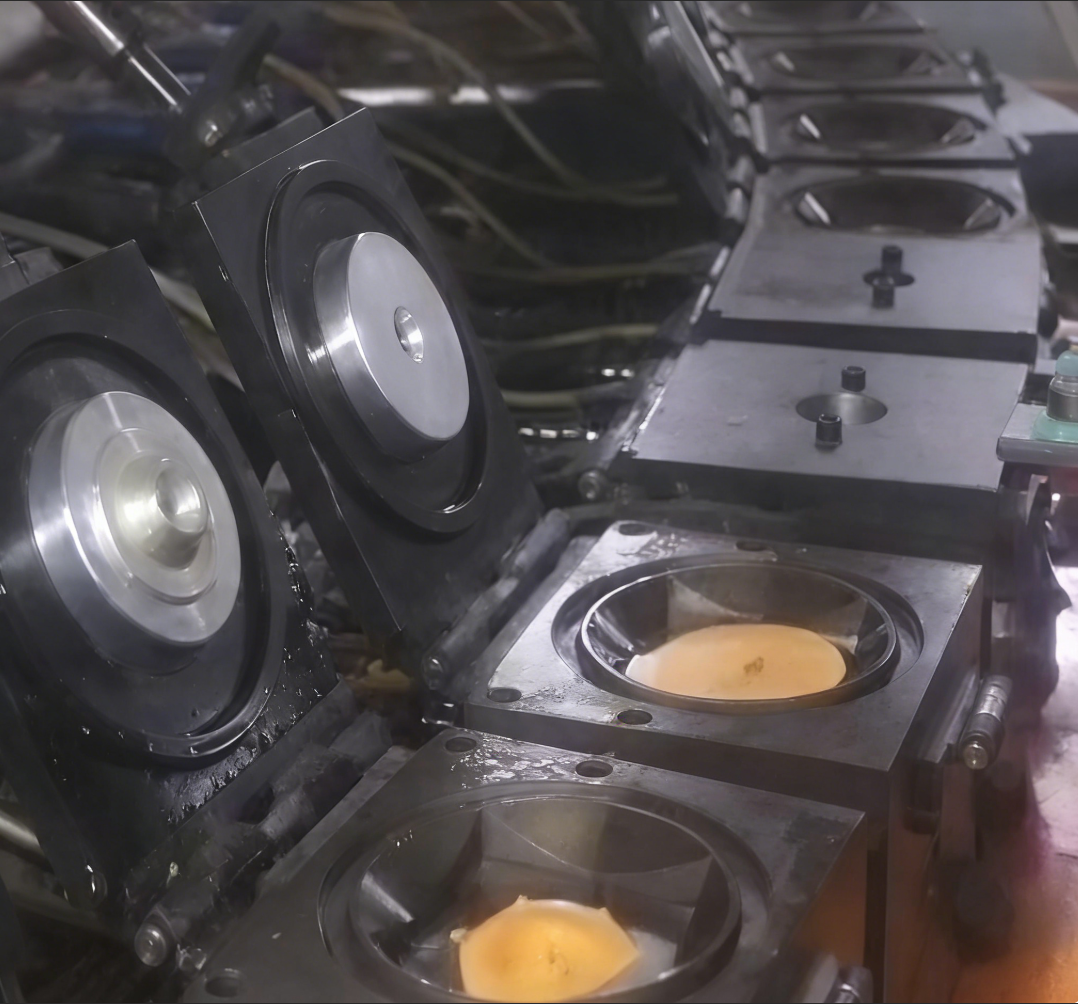
4 Mold automatically closes
5 Setting and curing
6 Mold automatically opens
7 Part removal, trimming, quality inspection, packaging

Equipment List and Unit Price

No. Name Quantity Dimensions Unit Price (USD)
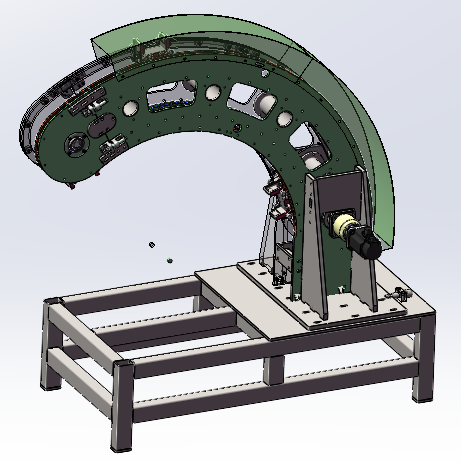
1 Mold Opening/Closing Machine 2 Sets Approx. (Unit mm)
1100×760×1000
2 Release Agent Spray Gun 1 Set Approx. (Unit mm)
105×155
Air Blow Gun 1 Set Approx. (Unit mm)
105×155
3 Automatic Release Agent Spraying Machine 1 Set Approx. (Unit mm)
1100×760×1000
4 Low Pressure Foaming Machine (2A2B) 1 Set Approx. (Unit mm)
1500×1500×2700
3-Axis Automatic Pouring Machine 1 Set Approx. (Unit mm)
3000×1500×2700
5 Heating Device (Mold Temp. Controller) 1 Set Approx. (Unit mm)
900×600×1100
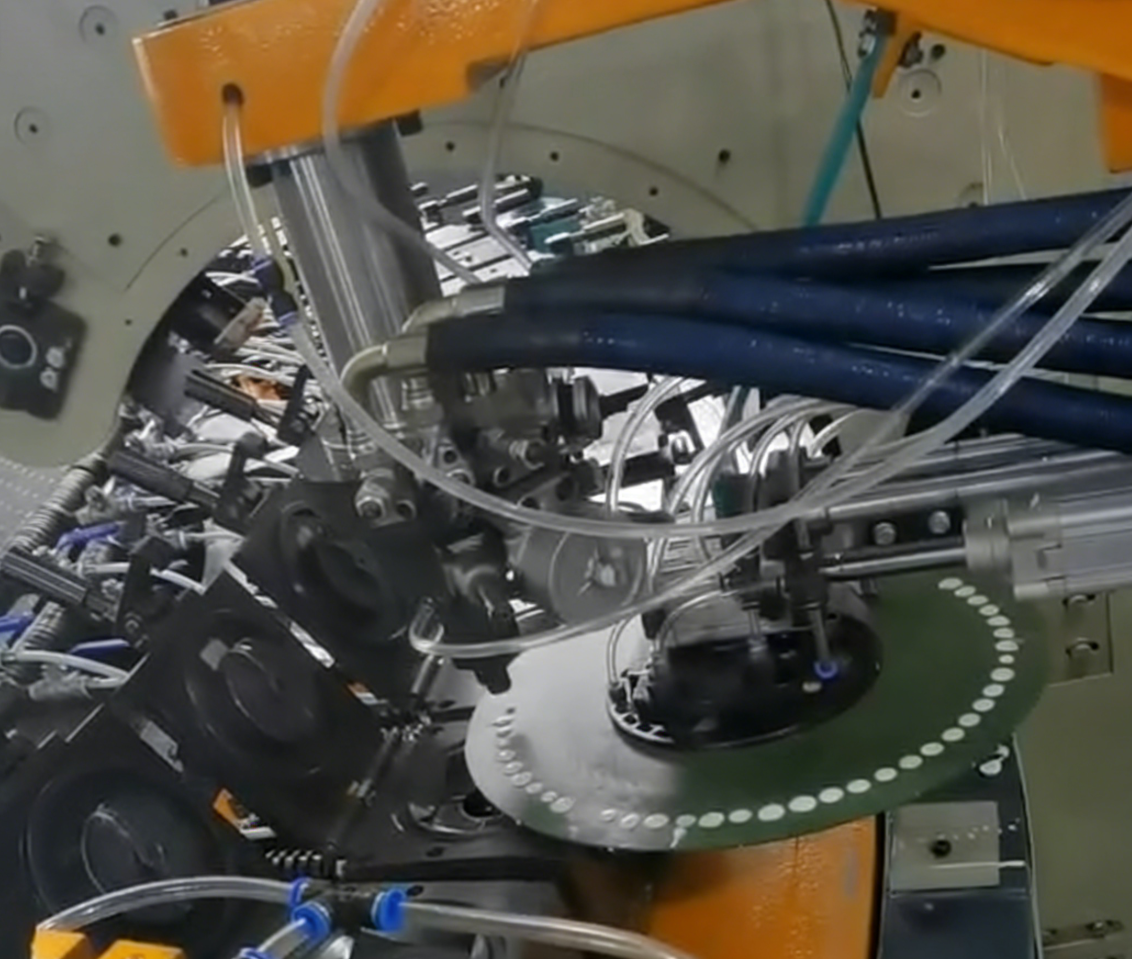
6 108-Station Rotary Disc Machine 1 Set Approx. (Unit mm)
9200 × 9200 × 2350mm
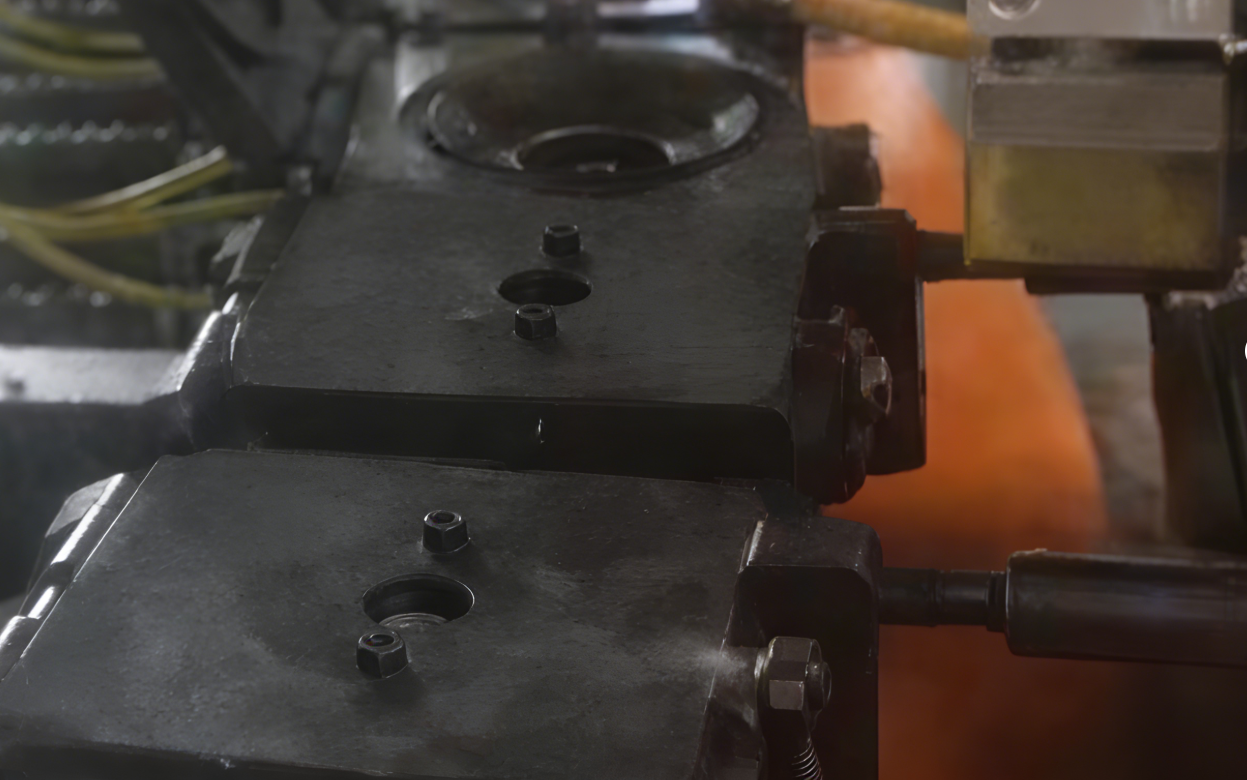
7 Mold Frame 1 Set Inner size 90*90, Total 108 pcs
Auxiliary Equipment
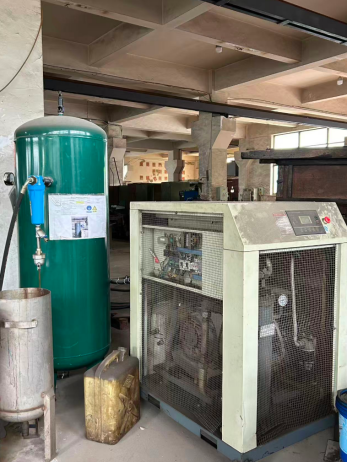
1 Air Storage Tank
(Prepared by Customer)
1 Set Approx. (Unit mm)
500×500×2000
Air Compressor
(Prepared by Customer)
1 Set Approx. (Unit mm)
1800×1000×2000
* The basic air consumption required for our company’s equipment. The air storage tank requires a single supply and should be close to the equipment.
2 Cold Dryer 1 Set Approx. (Unit mm)
900×600×1100
3 Raw Material Drying Oven 1 Set Approx. (Unit mm)
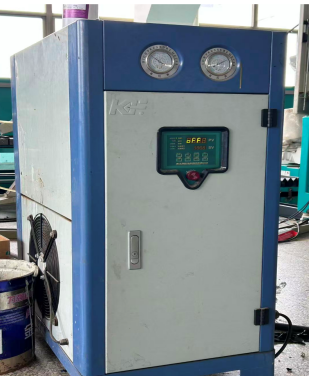
4 Chiller 1 Set Approx. (Unit mm)
900×600×1100
EXW Total Price
Shipping: 2×40′ Container

Configure Directory Table of Contents

Category Component Name Model / Spec Remarks
Pouring System Metering System Component A: 20cc High-precision metering pump Motor is 1.3KW servo motor with planetary reducer
Component B: 20cc High-precision metering pump
Color Dosing System 0.6cc High-precision metering pump Drive motor is 0.75KW servo motor, 50L storage tank
Gantry System Left-right data movement Movement motor is 1.3KW servo motor
Up-down data movement Movement motor is 1.0KW servo motor
Mixing Head System Needle valve mixing head With independent cooling system
Temperature Control System Hot water tank
Material tank temperature Independently control material tank temperature
2 HP Water Chiller Mixing head cooling
Mixing Head Cleaning System 20L cleaning tank
Machine Frame Assembly Frame structure
Control System PLC & Modules Brand: Shenzhen Inovance H3U series PLC & modules
10-inch Touch Screen Brand: MCGS
Low Voltage Electricals Brand: DELIXI
Sensors Brand: Inovance
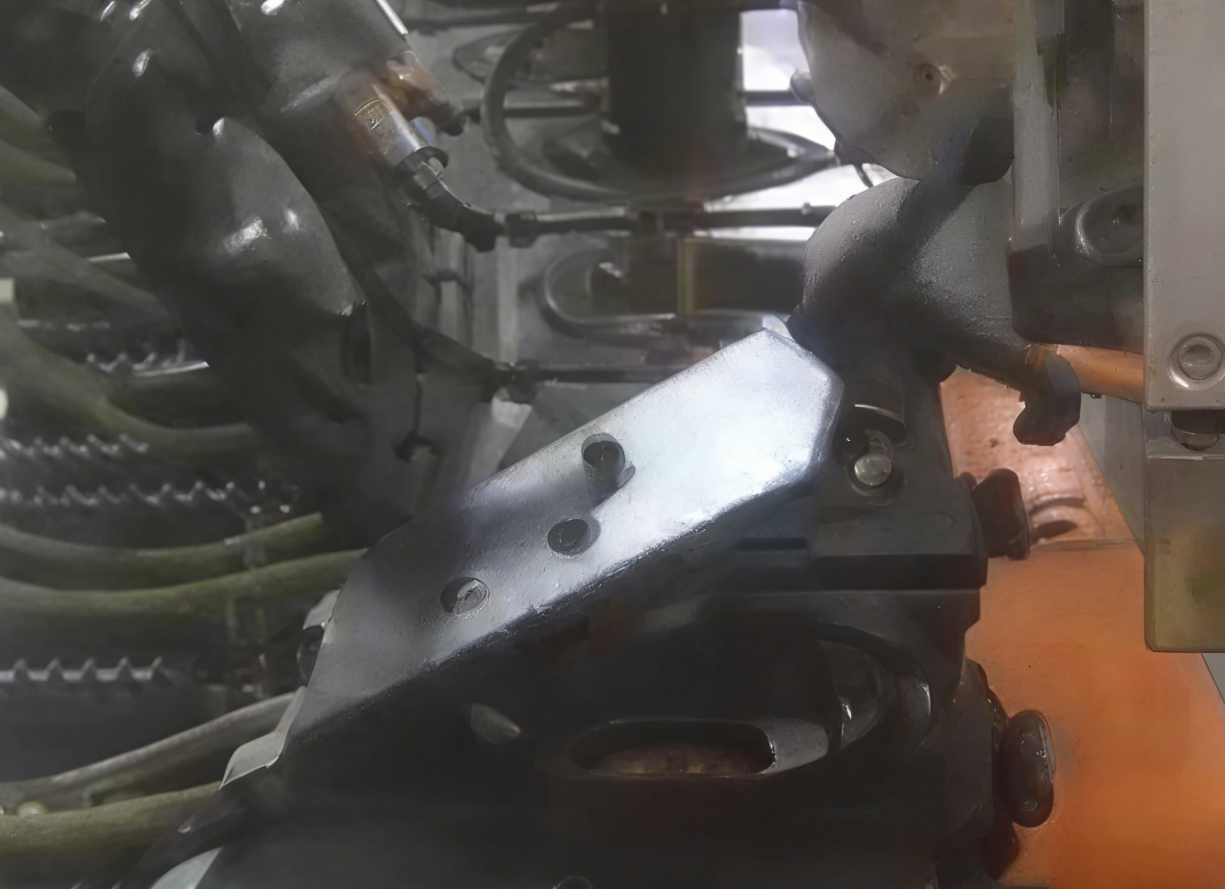
Mold Opening/Closing Machine Pneumatic cylinder drive opening/closing mold Cylinder stroke: determined by mold weight and required force
Stroke: depends on mold opening angle and height, generally upper mold opening angle needs ≥90°
Mold Release Spray Gun Model: MRS-R/F, Brand: Taiwan Baoli, Nozzle size ±20 Air pressure: 2.0Mpa, Weight: 320g
24-Station Polyurethane Carousel Line Overall dimensions: Total length approx. 8 meters, Number of stations: 24

Technical parameters

mould
Function: First select the mold for the product to be manufactured
(standard mold). Materials: Aluminum alloy, Cr12MoV alloy, tool steel.
The mold measures approximately 90
mm in length, 90 mm in width
and 146 mm in thickness.
Oven system
Function: Raw material oven for preheating and drying of AB material.
Model: XHG×3-2.5; Volume: 2.5 m³;
Temperature range: 90°C;
Temperature control mode: Automatic;
Total power: 6.55 kW.
Automatic opening and closing die machine
Function: Automatic mold opening and closing
Power (KW): 2
Coiling device system
Function: Automatic application of release agent before mold pouring
Function: When the cavity is relatively complex, manual supplementary spraying may be required.
gating system
Function: The casting machine performs casting based on the selected formula.
Maximum instantaneous flow rate: 40 g/s, rated voltage V: 380 V
108 automatic conveyor lines
Function: Supports the mold’s uniform cyclic operation.
Total power of the production line: approximately 85 kW.
cooling-water machine
Function: Cooling power for the pouring head and mixing
chamber kW: 1.91 kW
air pump
Functions: Cleaning and valve control provide power and
cooling source pressure for the pneumatic system and nozzle cooling
(requires continuous power supply). Power: 22 kW
Production output and production efficiency
Production Mode 108 Stations 77 Stations
Production Cycle
Production cycle per station is approx. 5-6 seconds.
Different mold cavities, process temperatures, and material characteristics may cause variations in cycle time.
(108 Stations)
Production cycle per station is approx. 5-6 seconds.
Different mold cavities, process temperatures, and material characteristics may cause variations in cycle time.
(77 Stations)
Avg. Time per Rotation Approx. 9-11 minutes Approx. 6.5-8 minutes
Hourly Output ≈ 590-720 pcs ≈ 580-710 pcs
Daily Output (8 Hours) ≈ 4720-5760 pcs ≈ 4640-5680 pcs
Working Conditions
Project Requirements
Workshop Requirements Level ground (Area approx. 11m × 11m), Power supply, Compressed air, Cooling water, Ventilation
Temperature & Humidity ≤40°C, Non-condensing environment
Power Supply 3×380V ± 5%, 50Hz, Reliable grounding (Provided according to actual site needs)
Operators 2-3 trained operators (Including pouring control, sampling, trimming, air blowing)

Full-Process Automated Production System

Integrated production line

Provide customized complete production lines covering all processes from raw material pretreatment to intelligent sorting. Core equipment adopts Haifeng’s independently developed imported configuration, ensuring material mixing uniformity ≥98% and stable and reliable operation.
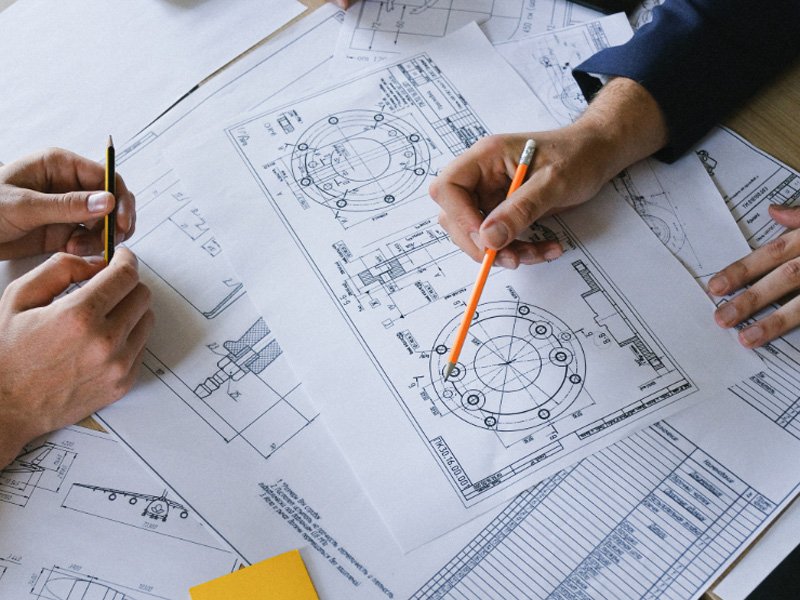
Customized adaptation

Rely on the CAD modeling and 3D printing capabilities of the Mechanical Design Research Institute to quickly produce customized molds and non-standard components, shortening the R&D cycle of new styles to 7-10 days.
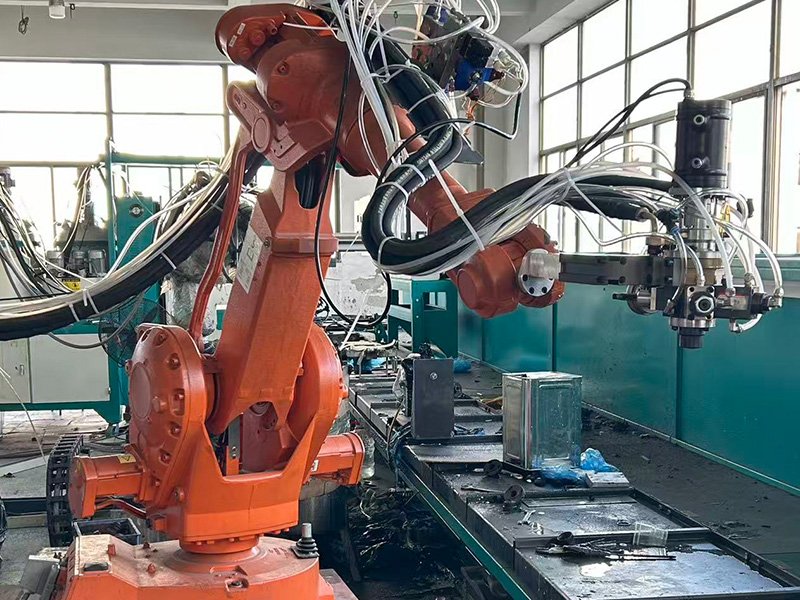
Existing equipment transformation

Install Haifeng’s intelligent temperature control, precision proportioning, and automated conveying modules to realize the transformation from solvent-based to solvent-free/water-based processes, reducing labor and raw material losses.
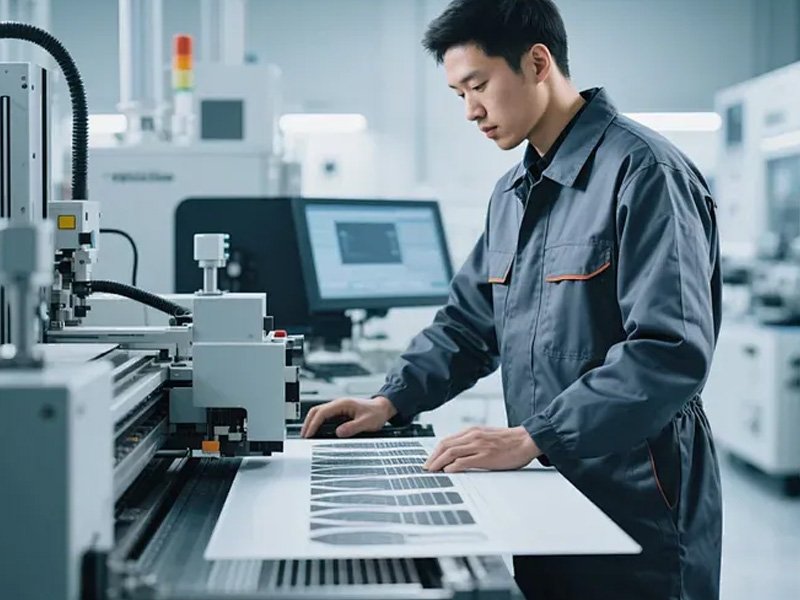
Comprehensive Quality Verification and Compliance Assurance

Intelligent quality inspection

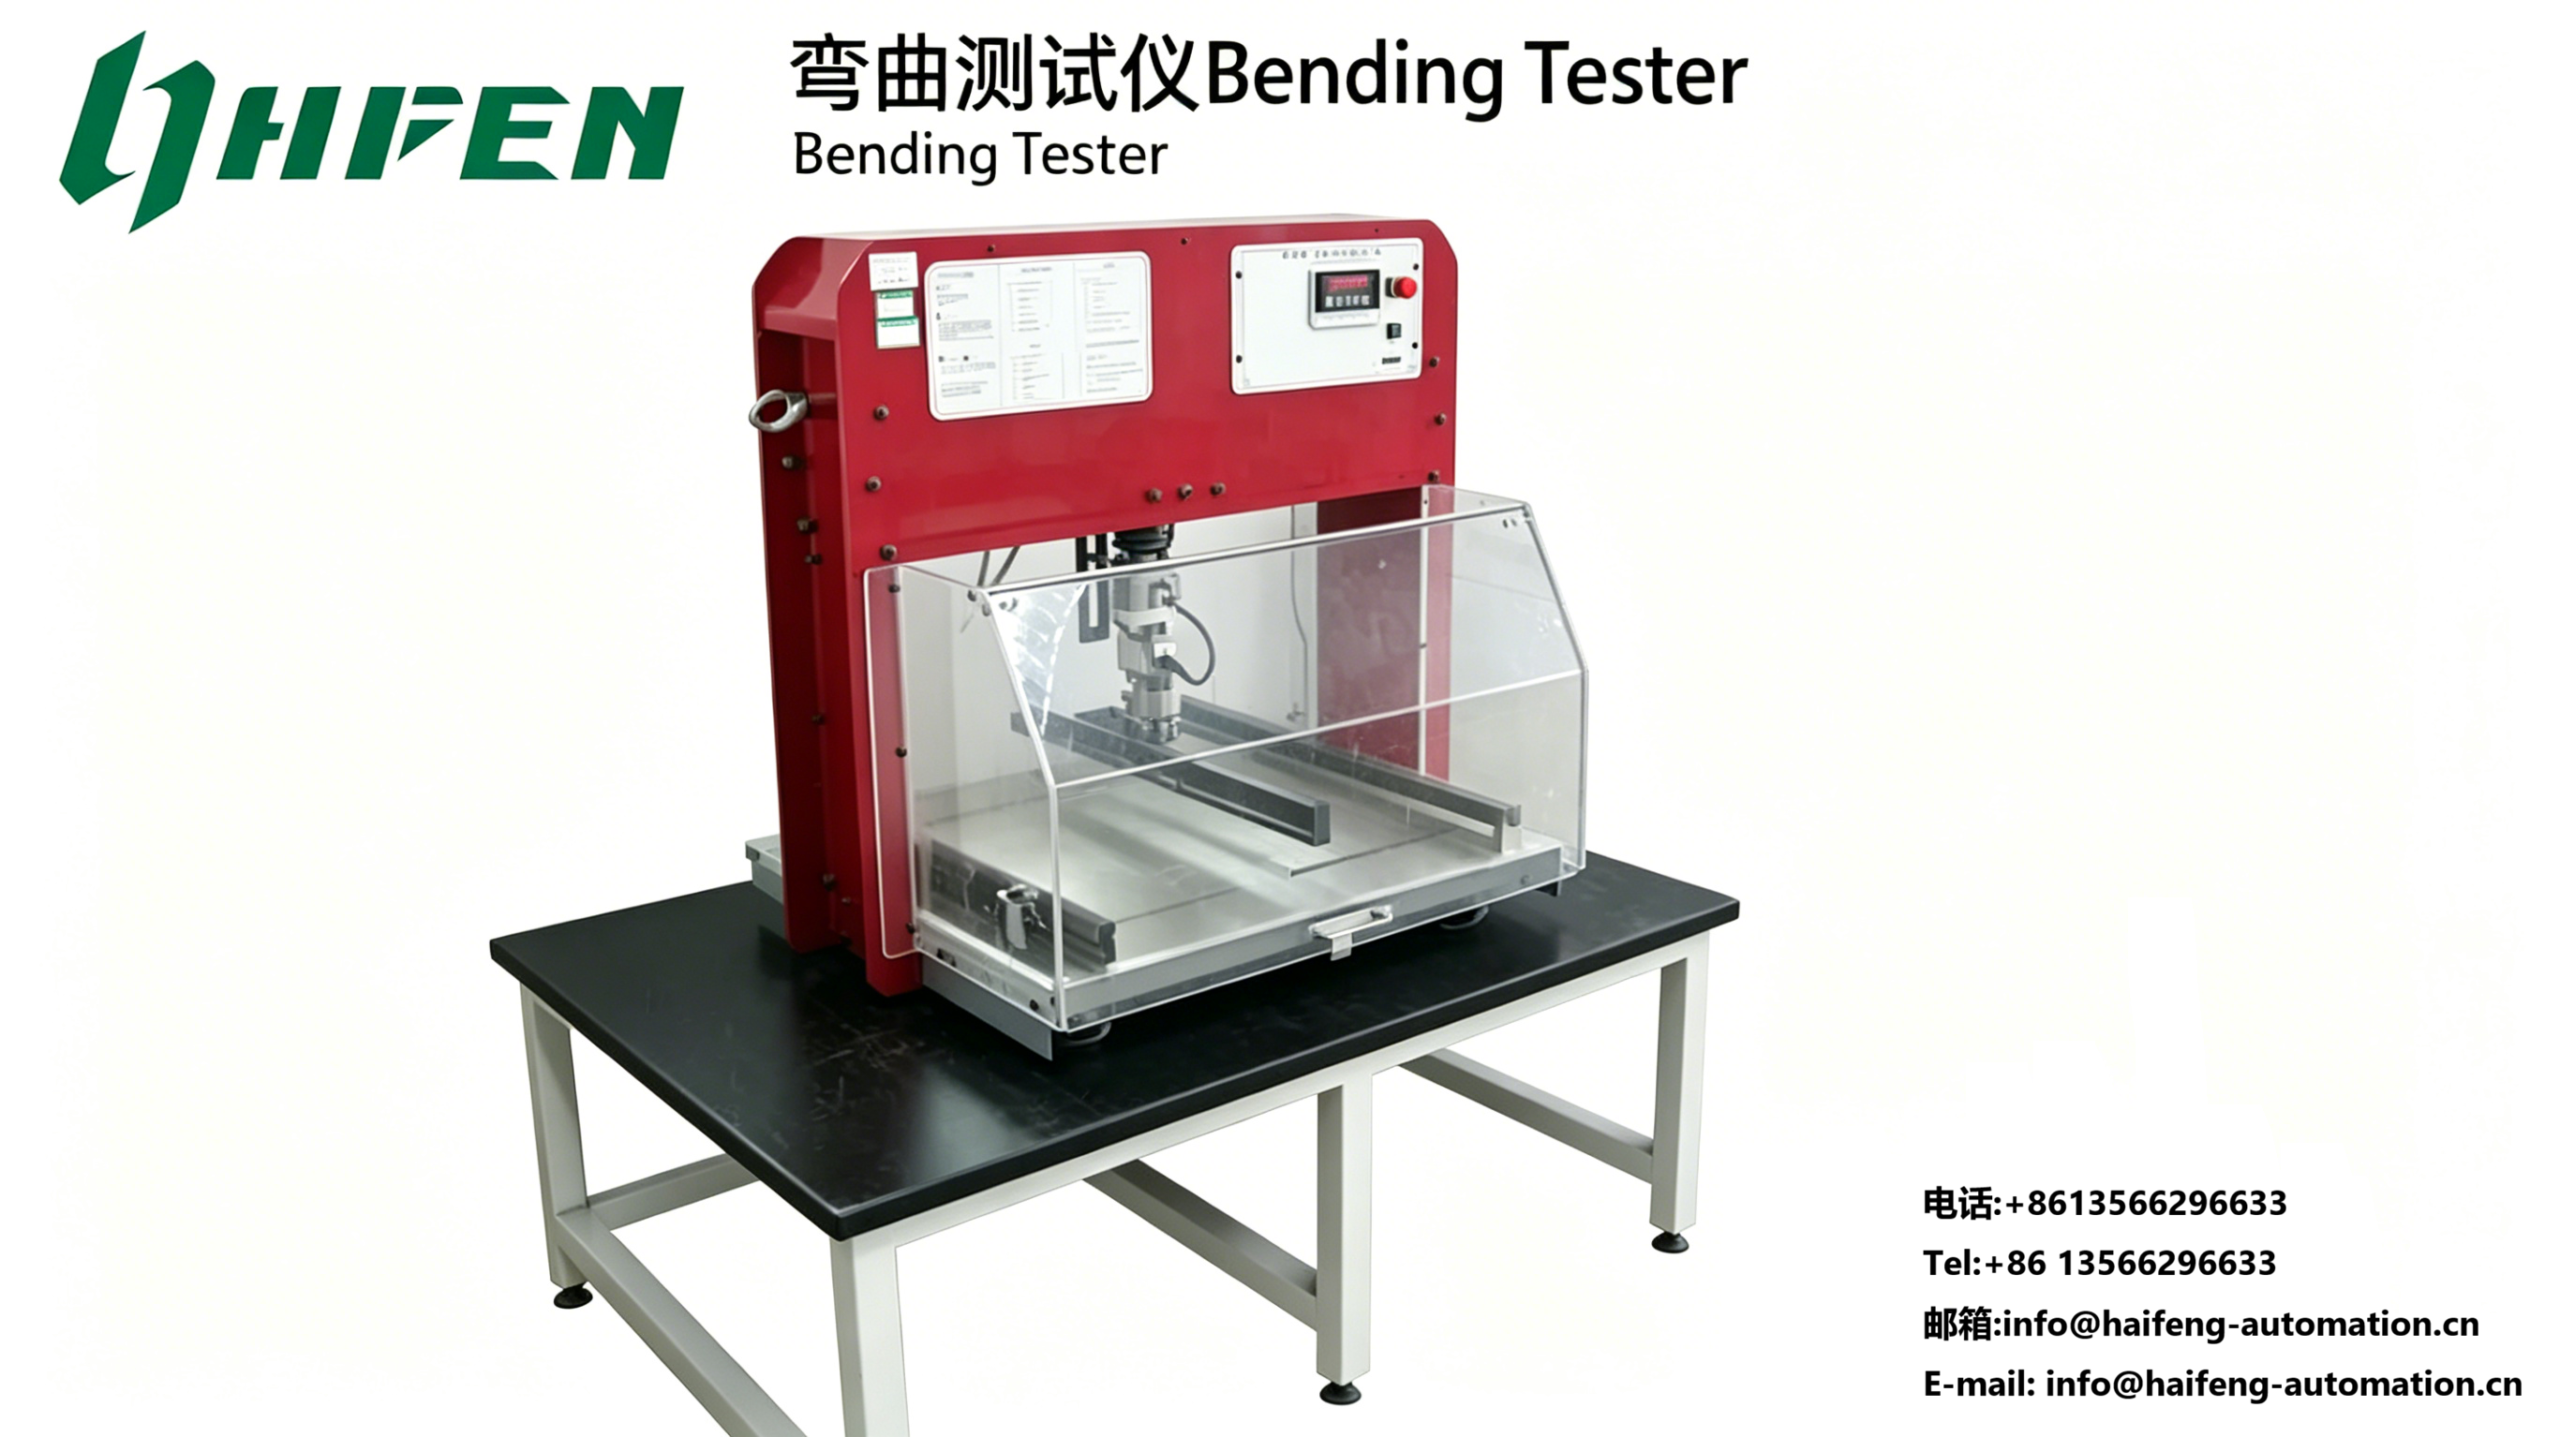
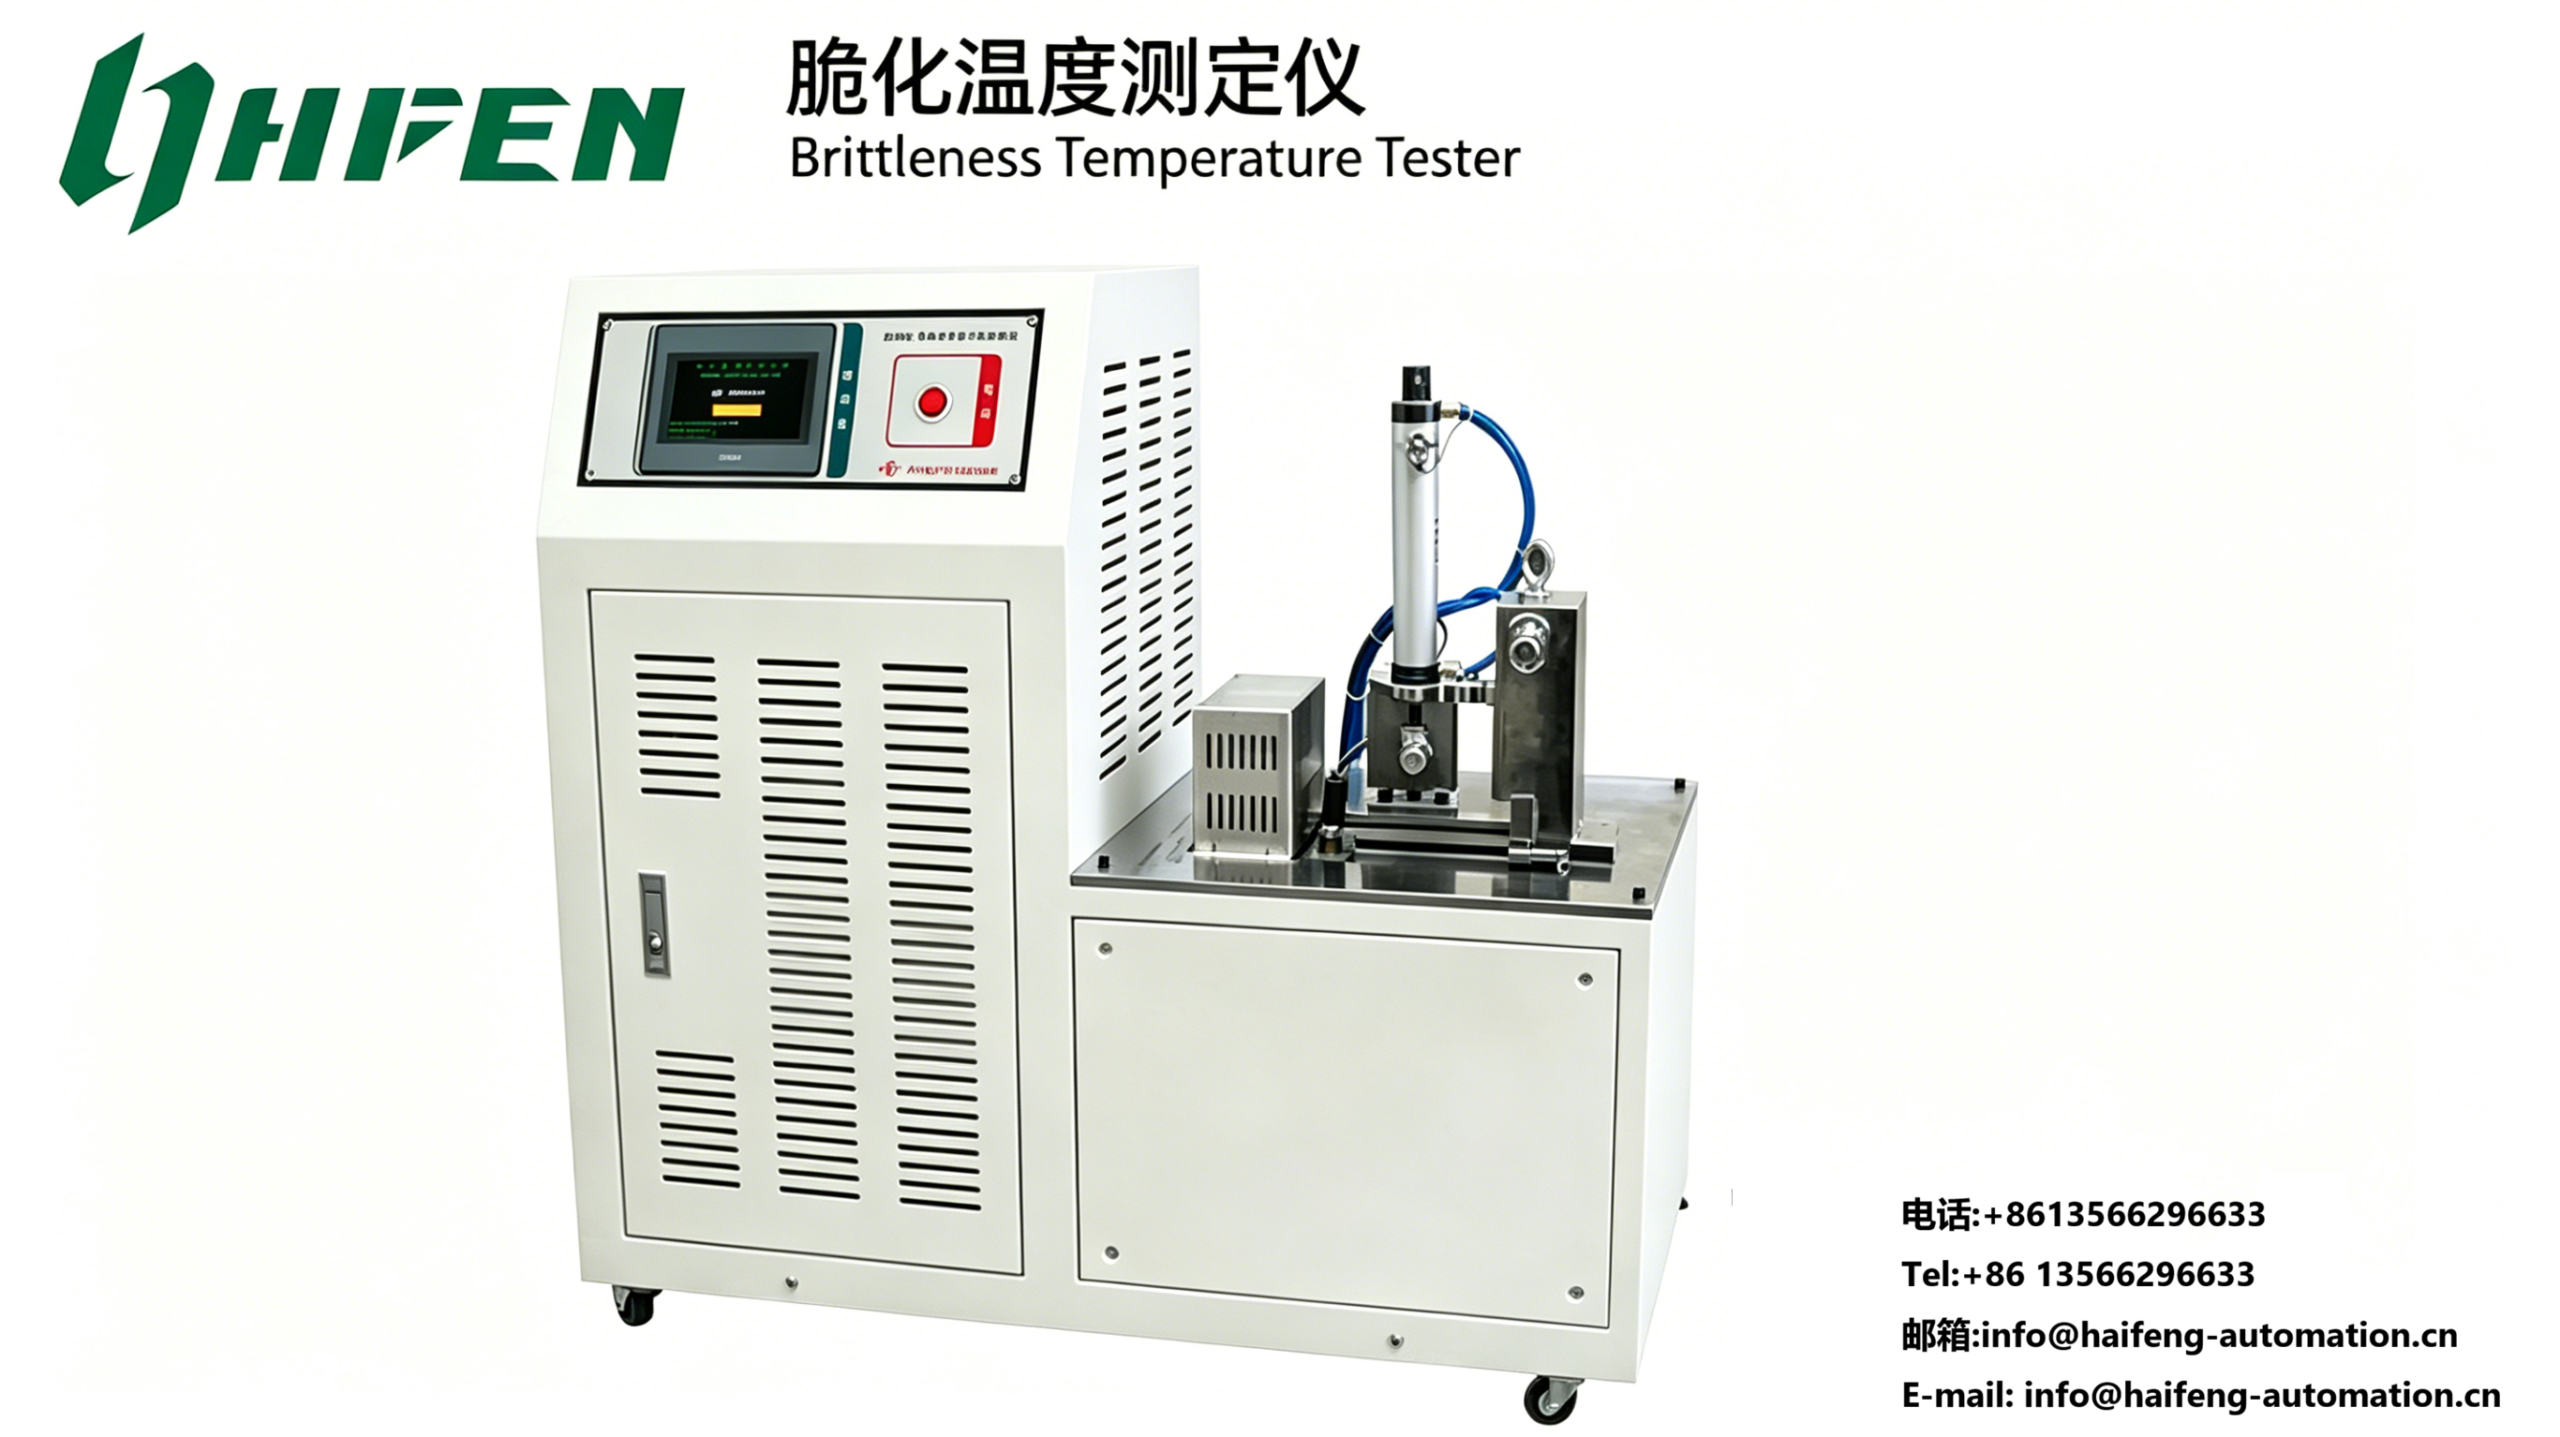
Equip Haifeng’s independently developed integrated testing equipment, covering thickness, defect, bonding strength, and key performance tests. With an efficiency of ≥50 pairs per minute, defective products are automatically sorted out.
Real-time control

Adopt Haifeng’s intelligent production control system to dynamically adjust parameters, controlling the defect rate at 2-3%; integrate environmental monitoring modules to achieve near-zero VOC emissions.
Certification support

Cooperate with authoritative testing institutions to assist in completing multi-standard certifications, providing technical parameters and sample support to help obtain CE and LA certifications and break through high-end market barriers.
Solution Value and Effects

Dimension Traditional Process Haifeng Automation Solution Improvement Effects
Compliance Rate of Protective Performance Below 85% Above 99% Meet national/international standards and eliminate safety hazards
Defect Rate 10-15% 2-3% Reduce by over 75% and minimize rework losses
Raw Material Waste Rate ≥15% ≤5% Reduce by 67%, saving over 300,000 yuan in raw material costs per line annually
Labor Requirement 8-10 people/line 2-3 people/line Reduce by 75% and lower the risk of operational errors
VOC Emissions Excessive Near zero Achieve environmental compliance and obtain international certifications
R&D Cycle 30-45 days 7-15 days Shorten by over 60% for rapid market response

Implementation Process

Demand Research

Technical team conducts on-site investigations to formulate personalized solutions.

Formula and Process Design

Complete customization and feasibility verification relying on the R&D Center.

Equipment Customization/Transformation and Commissioning

Factory completes production, with engineers conducting on-site installation and commissioning.

Small-Batch Trial Production

Technical team tracks and optimizes parameters.

On-Site Installation and Mass Production

Implement the production line and start mass production, providing technical guidance.

Quality Inspection and Certification Support

Assist in completing testing and certification applications.

After-Sales Operation and Maintenance

Provide maintenance and upgrading services relying on the national service network.

RELATED PRODUCTS

RELATED NEWS

CONTACT US

To find out more about our products and solutions,please fill out the form below and one of our experts will get back to you shortly.

Please agree to the Privacy Policy before submitting.